Some time ago we talked on this blog about the accuracy grades of gear teeth, highlighting how important it is because, when it is not indicated on a drawing, it can generate ambiguity and incorrect interpretations that will inevitably compromise the end result.
This is why I think it is important to recap this subject once again.
The accuracy grade of a gear can basically be considered as the combination of all the tolerance limits, i.e. all the admissible deviations from the absolute perfection of the main features of the actual teeth.
Based on this supposition, the American Gear Manufacturers Association (AGMA) has deemed it essential to qualify the range of such tolerance limits, to make it easier to define, at a general level, the actual accuracy of these components using progressive numbering that ranges from 3 to 15, where 15 is the most accurate gear and 3 the least accurate.
Apart from this range of admissible errors, no further grading of gears was deemed necessary. Below is a comparative table that shows the various interpretations given to this standard by different Countries.
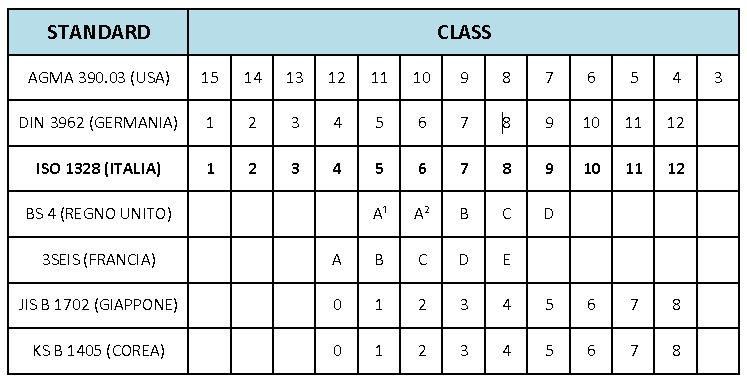
According to the Italian and German standard – and this is the most important observation – the maximum accuracy grading starts from the lowest number, i.e. the exact opposite compared to the requirements of the AGMA standard.
This second table, on the other hand, shows the errors that are taken into account by the ISO Standard 1328 (paragraphs 1 and 2).
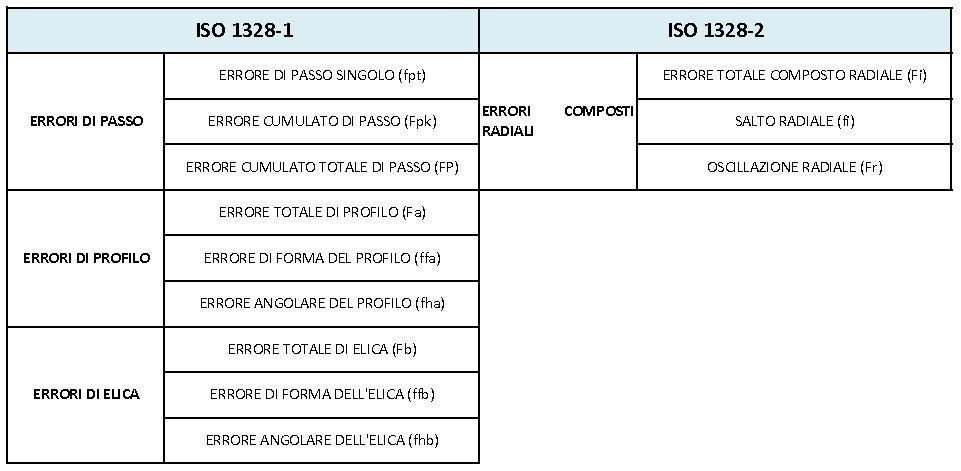
I would therefore like to emphasise once again that, in addition to the table describing the characteristics of the teeth and, if applicable, the surface roughness, indication of the accuracy grade will suffice (for example: ISO1328 accuracy grade 8) to uniquely identify all the admissible tolerance limits which avoids ambiguous interpretations and simplifies the actual realization of the products.
In my next posts I would like to run through the accuracy grades of some typical applications and how the productive typologies of a gear impact the accuracy grade.